Tel.: +86 136 7029 7045
Contact Us >

EN

Engineering a More Durable Balloon Mold

Material, Surface, and Design Optimization for Long-Term Production Reliability

From premature surface deterioration and mounting failure to 24,000+ hours of reliable production.


Engineering a More Durable Balloon Mold

The Challenge

A Production Mold That Could Not Withstand Continuous Operation


A balloon manufacturer approached TC Precision after experiencing repeated failures with stainless steel molds supplied by another machining shop. The customer needed more than a replacement mold. They needed to understand why the original design and manufacturing process were failing and how to develop a solution suitable for continuous production.


Two Critical Functions


The mold had to meet two essential requirements:


1 Maintain a stable molding surface because the surface directly forms the latex film.

2 Maintain a reliable mounting structure because the mold is subjected to continuous mechanical loading on the production line.


Original Performance Requirements


The customer required a functional surface with Ra 0.4 μm roughness, resistance to the corrosive latex compound, easy cleaning, and long-term dimensional and surface stability.


Failure 1: Surface Deterioration


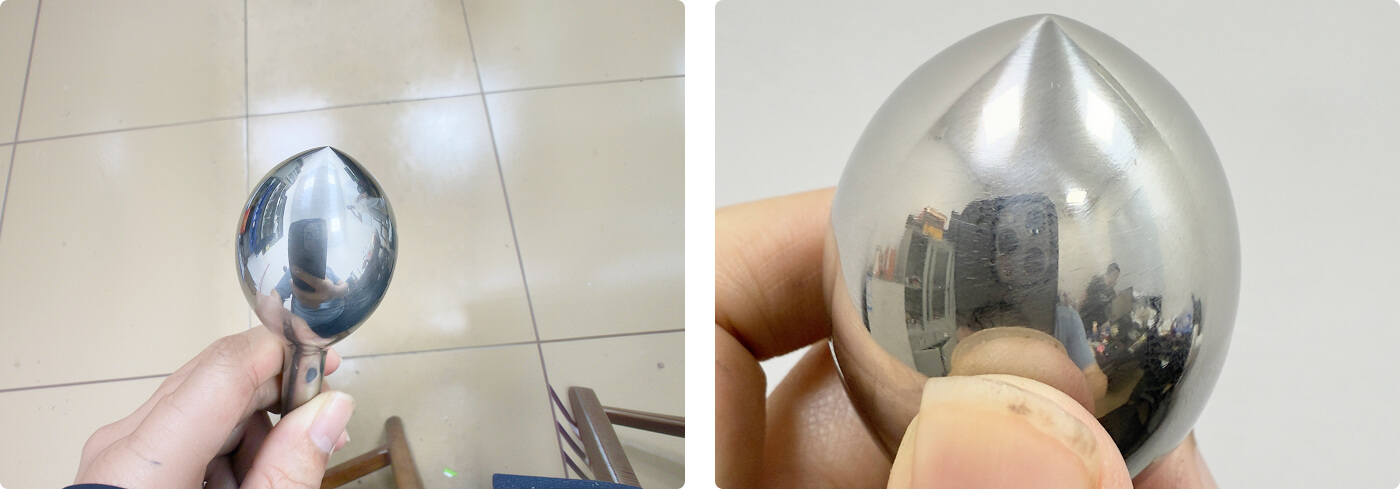
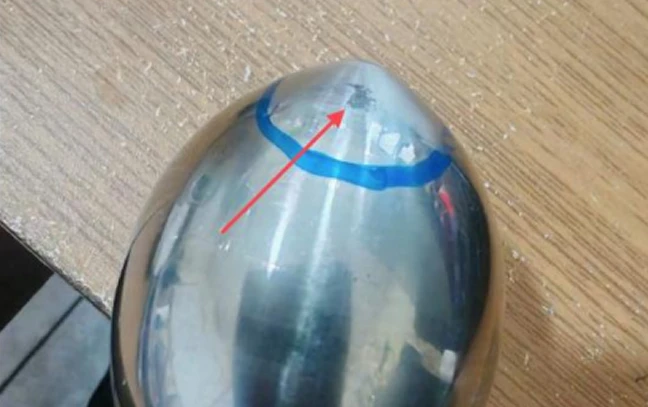
Localized deterioration appeared on the mold surface after the molds entered production. The affected area showed characteristics resembling pitting, flaking, or loss of surface finish.


Because the surface directly forms the balloon, any local change in roughness could transfer to the latex film and cause visible marks, thickness variation, residue buildup, adhesion problems, or weak points.


Failure 2: Mounting Joint Separation


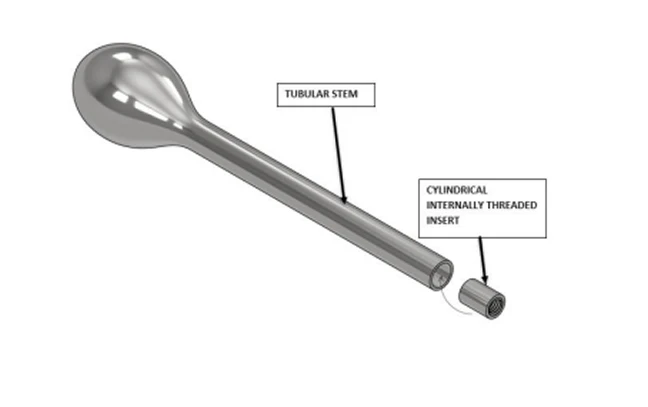
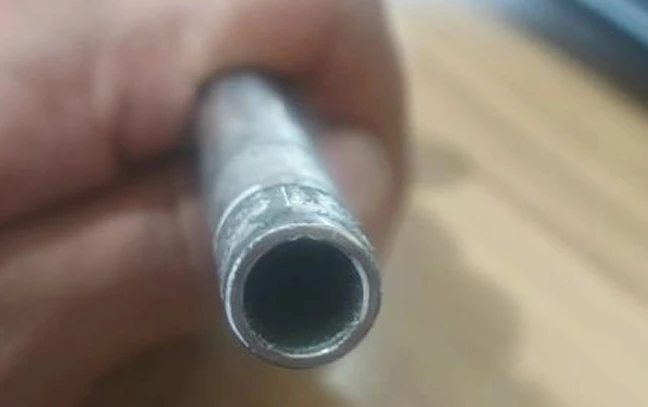
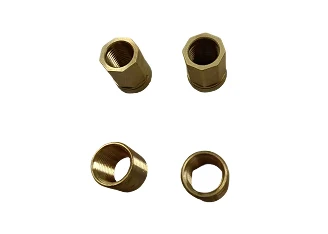
The original mold used a tubular stem with a cylindrical threaded insert welded to its end. A screw then secured the mold to the production frame.


During operation, the welded insert detached from the stem while the insert and screw remained attached to the machine frame. All three molds experienced this failure within 24 hours of entering production, confirming a repeatable and premature joint failure rather than an isolated defect.

Project Overview

Item Details
Industry Industrial Automation / Latex Balloon Manufacturing
Part Stainless Steel Balloon Production Mold
Application High-volume balloon production
Material 316L Stainless Steel
Processes Sheet Forming · Welding · CNC Turning · Mechanical Polishing · Electropolishing
Production Quantity 10,000 pcs

Engineering Review

Identifying the Root Causes Across the Manufacturing System

Our objective was to improve both surface durability and mechanical reliability without compromising the mold geometry.

We reviewed the original CAD model, manufacturing sequence, material selection, welding structure, machining requirements, polishing process, and mounting method.


Original Manufacturing Route

Sheet Forming → Welding → Mechanical Polishing


Our review identified three major engineering risks.

Forming Alone Could Not Fully Reproduce the Mold Geometry

Risk 1: Forming Alone Could Not Fully Reproduce the Mold Geometry

The original process relied on sheet forming to create the main semi-circular shape.

However, forming could not consistently reproduce the fine three-dimensional features required at the top of the mold.


If the final geometry depended entirely on forming accuracy and tooling conditions, the small features would remain difficult to control. Aggressive polishing could then remove material from these features and round or weaken them.


Engineering concern: More polishing was not the solution. The more material removed during polishing, the greater the risk of changing the fine geometry.

Material and Surface Treatment Had to Be Considered Together

Risk 2: Material and Surface Treatment Had to Be Considered Together

The mold operates in continuous contact with a corrosive latex compound and requires a stable, cleanable molding surface. Achieving the required initial surface roughness was not enough. The surface also had to maintain its condition through repeated production cycles.


Instead of treating material selection, machining, and surface finishing as separate decisions, we evaluated them as one manufacturing system:

The Mounting Joint Relied Too Heavily on the Weld

Risk 3: The Mounting Joint Relied Too Heavily on the Weld

The original mounting design placed the threaded insert at the end of the tubular stem and relied on the welded joint to carry the operating load.


This meant that the weld served as both the joining method and the primary load-bearing structure. For a component exposed to continuous production-line loading, this created a mechanical fatigue risk.


The production failure confirmed the concern: the insert separated from the stem while the insert and screw remained attached to the machine frame.


Engineering principle: Use the mechanical structure to carry the load—not the weld alone.

Have an Engineering Challenge?

Let’s Solve It Together.

From engineering review and design optimization to prototyping, low-volume production, and scalable manufacturing, TC Precision provides the expertise and manufacturing support you need to move forward with confidence.